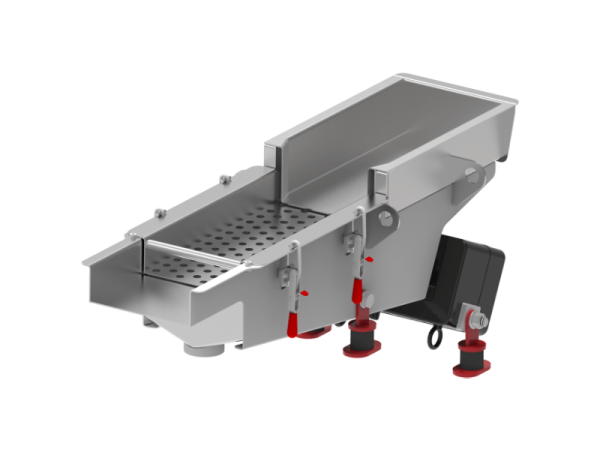
Vibratory equipment for the chemical industry
At SINEX, we understand that each project in the chemical industry is unique.
That's why we offer customized solutions for the handling and screening of chemical products, taking into account the specific characteristics of each application, such as abrasiveness, acidity, humidity, temperature, and the presence of dust.
Our vibratory equipment for the chemical industry is available in steel or stainless steel, and is designed to meet the most stringent quality standards, including ATEX certification for explosive environments.
Examples of products we handle for the chemical industry:perchlorate, catalysts, granules, PVC, pellets, rubber, detergent, nitrates, caustic soda, sulfate, plastic granules, paint additives, TSP, DCP, MCP, urea, calcium carbonate, fertilizers
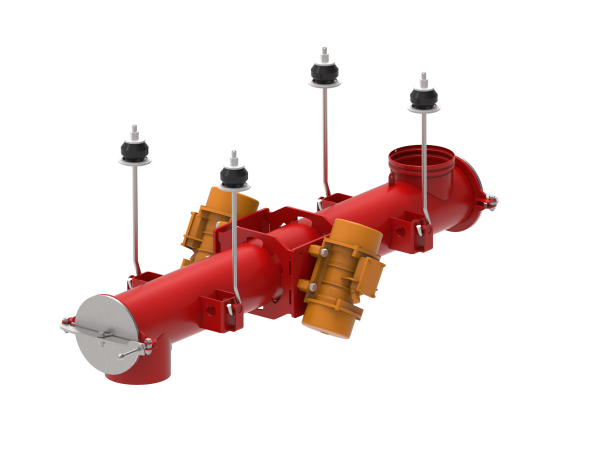
Electromechanical Vibrating Tubular Conveyor
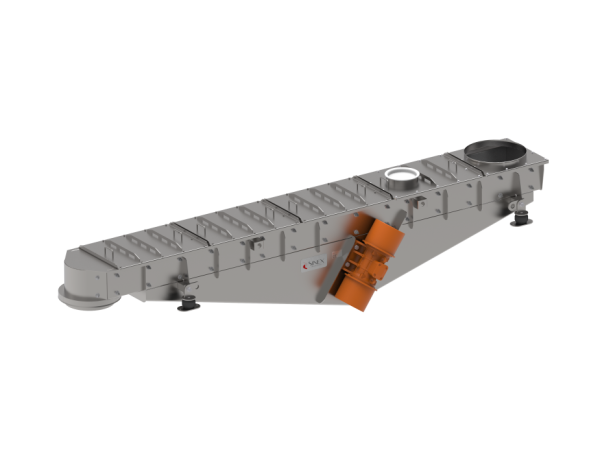
Electromechanical Rectangular Vibrating Conveyor
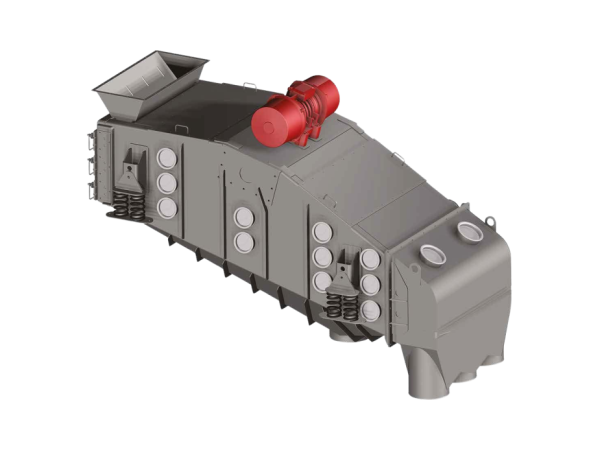
Electromechanical Vibrating Sieve
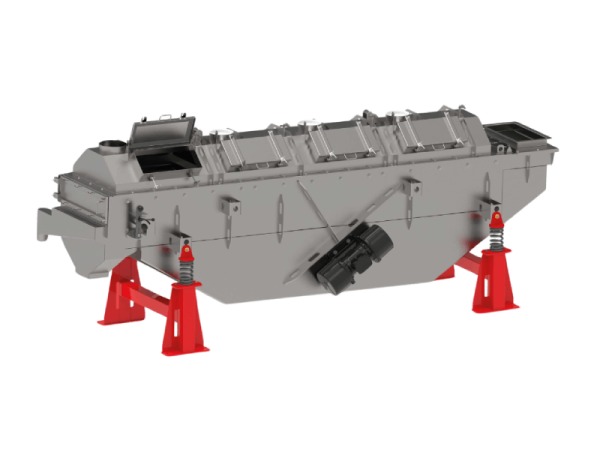
Fluidized Bed Dryer
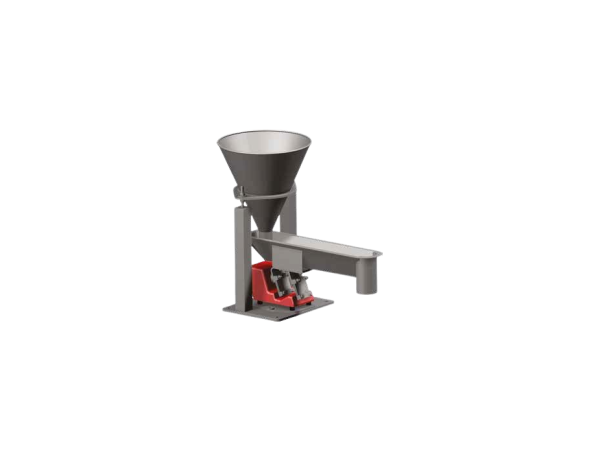
Electromagnetic Vibrating Feeder
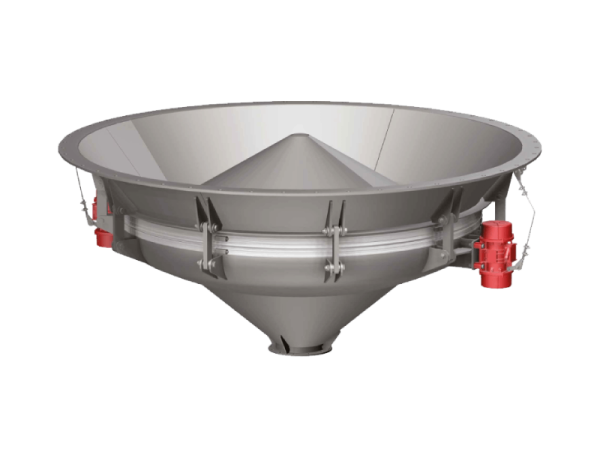
Vibrating Bin activator
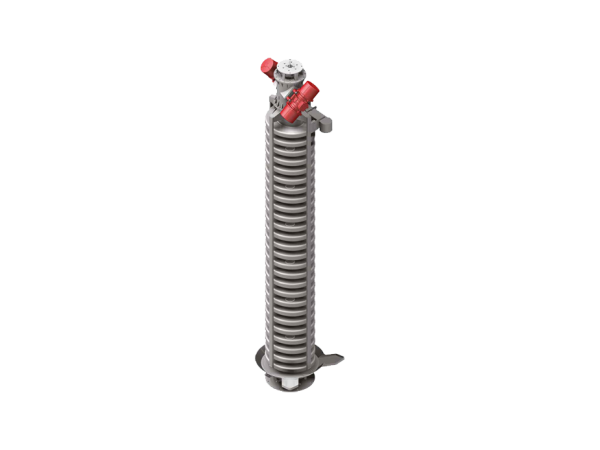
Vibrating Electromechanical Elevator
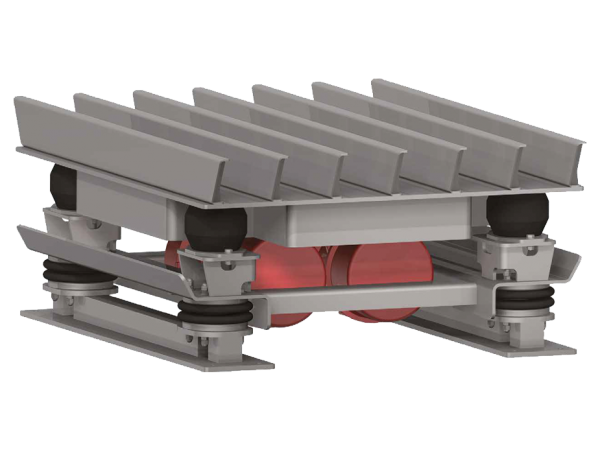
Vibrating Compaction Table
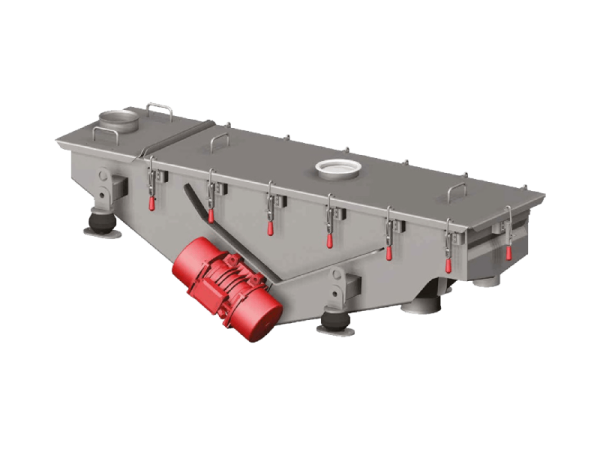
Electromechanical Vibrating Screen
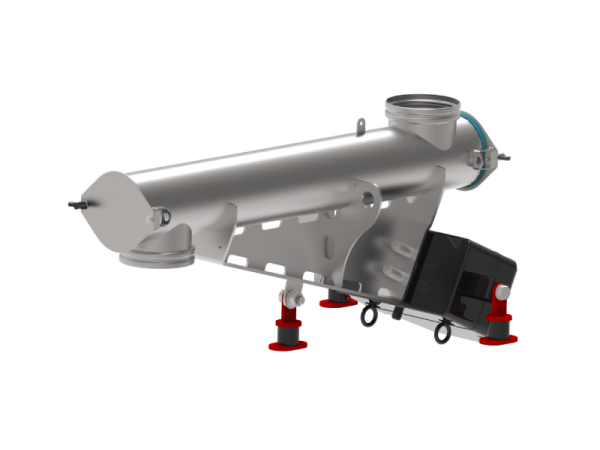
Electromagnetic Tubular Feeder
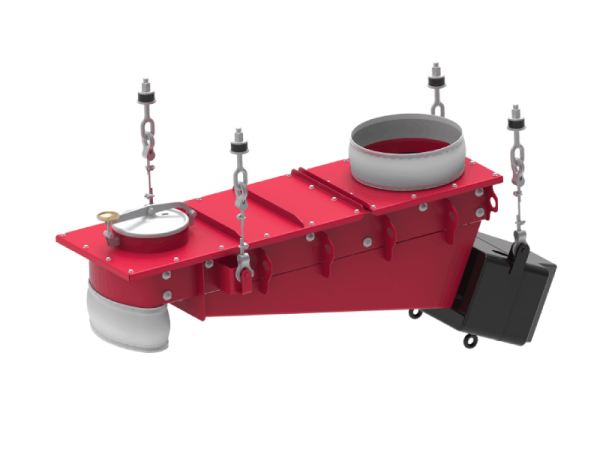
Electromagnetic Rectangular Feeder
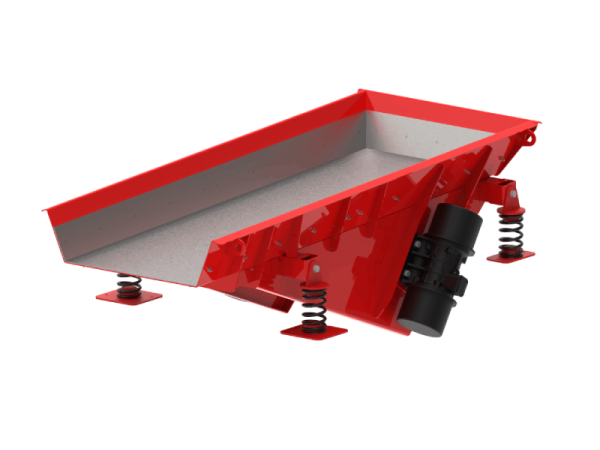
Extractor / Conveyor EME